
JY
JY-08 Single-Axis Headstock-Tailstock Welding Positioner Welding Positioner
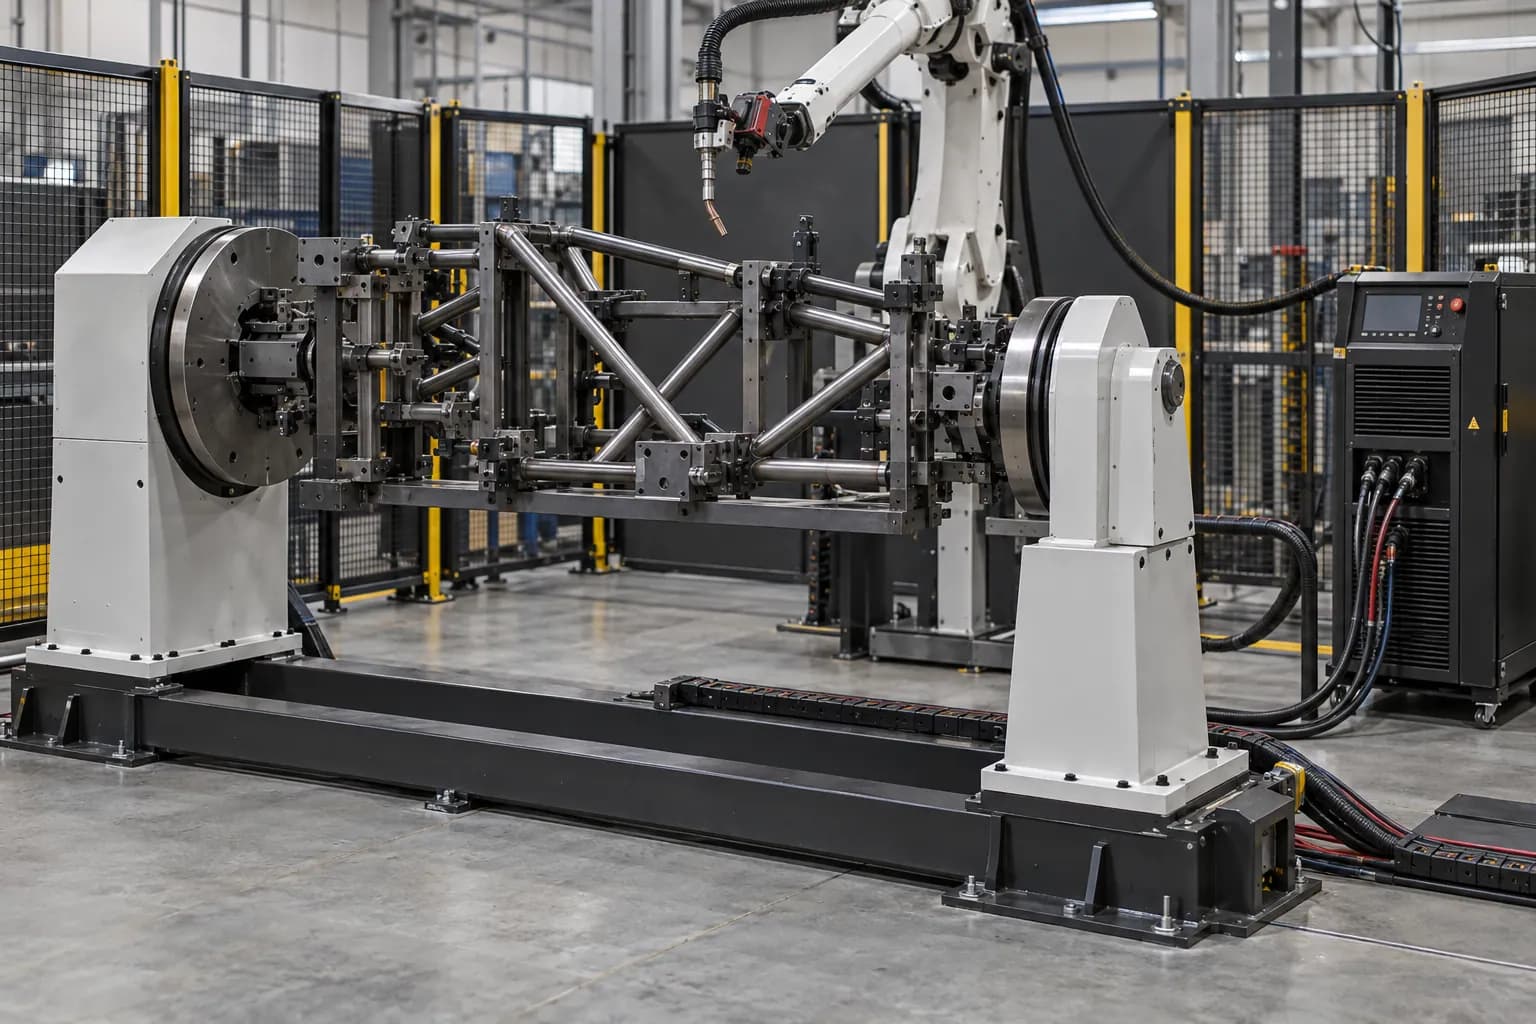
JY-08 is a single-axis headstock-tailstock welding positioner for fixtures supported between two ends. The 300, 500 and 1000 variants provide distinct load and rotation-radius combinations for comparing long weldment arrangements.
- Model options
- 3
- Compare by
- Support, axes and loaded geometry
Workpiece support and weld orientation
JY-08/300 and /500 list R690 mm rotation radii; /1000 lists R740 mm and a lower listed rotation speed. Include clamps and the complete fixture in the rotating envelope. Support spacing and off-center loading are drawing-dependent selection inputs.
A welding positioner changes the workpiece orientation so the torch can reach the joint in a suitable position. Choose the supporting structure first: a table, headstock-tailstock, trunnion or offset arm loads the mechanism differently. The moving assembly includes the part, fixture, clamps and attached services. Center of gravity, inertia and the distance from each axis are as important as nominal mass. Check the complete rotating envelope with doors, robot, cables and loading equipment. Decide whether the workpiece indexes between welds or moves in coordination with the robot during welding.
Application focus
- Robotic welding
- Fixture rotation
Specifications and selection notes
This page covers several models. The comparison below assigns each rating to its model; select an individual row before sizing the fixture, drive or installation.
Choose the model and configuration
Each row describes the named variant. Use its values together; parameters from different rows are not a combined specification.
| Model / arrangement | Technical data |
|---|---|
| JY-08/300 |
|
| JY-08/500 |
|
| JY-08/1000 |
|
Define what you need supplied
Single-axis rotation
Present joints around one workpiece axis with suitable fixture support.
Tilt and rotation
Change joint angle and presentation; check the offset load at both axes.
Multiple orientations/stations
Combine part orientation with a defined exchange and protected loading sequence.
Match the equipment to your installation
Provide anchoring, fixture attachment, welding return, services and clearance for the loaded mechanism. For coordinated motion, identify controller, servo/drive package, axis licenses and calibration responsibilities. Plan loading and recovery without reaching into moving equipment. Check each required orientation with the fixture fitted, including clamping, cable behavior and removal of the finished part.
| Selection factor | Information to specify |
|---|---|
| Loaded assembly | Workpiece and fixture mass, center of gravity, inertia and axis offsets. |
| Support geometry | Fixture mounting, support span, swing radius, clamp envelope and loading height. |
| Motion requirement | Indexing or coordinated motion, required angles, zero references and travel limits. |
| Services and access | Welding return, pneumatics, sensor cables, protection and finished-part removal. |
From the part to the equipment package
- 01Calculate the loaded fixture
- 02Choose support and axes
- 03Check every weld orientation
- 04Define drives and services
- 05Test rotation, loading and release
Tooling, interfaces and service access

Product and ordering questions
01What are the applications of JY-08 Single-Axis Headstock-Tailstock Welding Positioner Welding Positioner?+
JY-08 is a single-axis headstock-tailstock welding positioner for fixtures supported between two ends. The 300, 500 and 1000 variants provide distinct load and rotation-radius combinations for comparing long weldment arrangements.
02Can the rated load be used for any fixture offset?+
No. The complete part-and-fixture mass must be evaluated with its center of gravity, axis offset and inertia. A long or off-center fixture changes the load case even at the same mass. Provide the assembly drawing and required motion so the selected mechanism and drive can be checked together.
03What should I consider when choosing JY-08 Single-Axis Headstock-Tailstock Welding Positioner Welding Positioner?+
JY-08/300 and /500 list R690 mm rotation radii; /1000 lists R740 mm and a lower listed rotation speed. Include clamps and the complete fixture in the rotating envelope. Support spacing and off-center loading are drawing-dependent selection inputs.
04What should the equipment package include?+
Identify the selected equipment and separate the following packages: single-axis rotation, tilt and rotation, multiple orientations/stations. State which accessories, controls, installation, programming and commissioning are included. This makes equipment-only and integrated proposals comparable without assuming identical supply scope.
05How can I request a quotation for JY-08 Single-Axis Headstock-Tailstock Welding Positioner Welding Positioner?+
Send the required model or arrangement, quantity and destination, plus workpiece and fixture mass, center of gravity, inertia and axis offsets; fixture mounting, support span, swing radius, clamp envelope and loading height. Add photographs or drawings and identify existing equipment. TubeFrame can then discuss model sourcing, configuration and partner-supported integration as separately defined work packages.
Specify your next equipment package
Send the model or configuration, drawings, quantity and destination. We will discuss equipment sourcing, technical interfaces and any integration work required for your application.